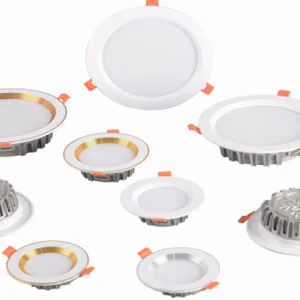
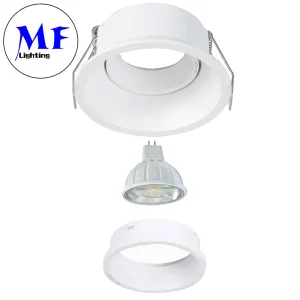
Explore our top-tier architectural, industrial, and specialized illumination products engineered for global commercial deployments.
As a leading Custom OEM LED Infrared Light Factory & Exporter, we bridge the gap between complex optoelectronic engineering and tangible industrial deployments. Our macro solutions span commercial architecture, agricultural growth lighting, secure surveillance infrared arrays, and heavy industrial automation.
Modern commercial spaces demand multi-functional lighting systems that integrate visible illumination with specialized infrared wavelengths for biometric security, touchless sensor networks, and automated environmental adaptation. Our ODM/OEM frameworks allow architectural designers to embed precise nanometer-wavelength emitters seamlessly.
In high-speed manufacturing lines, infrared LED emitters play a critical role in quality control, automated optical inspection (AOI), and localized adhesive curing. We engineer high-radiant-flux infrared modules that maintain thermal stability under extreme duty cycles, ensuring zero downtime for global production facilities.
Optimizing plant morphogenesis requires precise far-red and near-infrared spectra. Our custom horticultural lighting solutions stimulate phytochrome responses, accelerating biomass accumulation and flowering cycles in controlled environment agriculture (CEA) across greenhouse operations worldwide.
The global market for infrared and specialized LED solutions is undergoing a paradigm shift driven by IoT connectivity, automated security, and energy efficiency mandates. As an established Custom OEM LED Infared Light Factory & Exporter, we analyze macro trends to deliver future-proof manufacturing.
Operating out of Foshan, Guangdong—the lighting capital of the world—our ecosystem allows us to source premium electrical components seamlessly. We partner exclusively with tier-one component leaders such as TRIDONIC drivers and high-efficacy light sources from CITIZEN, BRIDGELUX, and CREE. This vertical integration insulates our international clients from supply chain volatility while guaranteeing exceptional luminous efficacy and thermal longevity.
Navigating international trade requires absolute adherence to regional standards. Our products are engineered and tested to satisfy rigorous global benchmarks including CE, EMC, ENEC, UL, and RoHS. Whether supplying high-end commercial real estate developments in North America or public infrastructure projects across Europe, our export team ensures streamlined customs clearance and zero-defect delivery.
Trust is built on verifiable quality and consistent execution. Our factory management systems operate under international environmental and safety standards to protect our partners and end-users.
We have proudly acquired OHSAS18001:2007 and ISO14001:2004 certifications, reflecting our unwavering dedication to occupational health, safety, and rigorous environmental management throughout our 15,000 square meter manufacturing facility.
Every commercial or industrial client has unique specifications regarding wavelength output (e.g., 850nm vs 940nm infrared), beam angles, housing dimensions, and thermal dissipation. Our dedicated R&D engineering team collaborates closely with clients from prototyping to mass production.
Before any product leaves our export docks, it undergoes rigorous burn-in testing, integrating sphere photometric evaluation, waterproof rating verification (up to IP65), and electrical safety checks to ensure flawless field performance.
As photonics and solid-state lighting evolve, our R&D roadmap focuses on next-generation efficiency, intelligent spectral tuning, and sustainable circular manufacturing.
Developing ultra-compact secondary optics that merge high-power infrared emitters with narrow beam divergence, ideal for long-range surveillance and high-precision industrial sensing without thermal degradation.
Integrating smart control protocols that allow dynamic adjustment of infrared and visible spectrum outputs in real-time, responding to environmental triggers and optimizing energy consumption across smart city installations.
Transitioning entirely to modular, disassemblable aluminum housings and recyclable packaging materials to fulfill zero-carbon manufacturing commitments well ahead of global regulatory deadlines.
Diva Lighting was founded in Foshan, China in 2000, with the idea of continuous innovation and strict quality control. The factory of Diva Lighting is located in Foshan, Guangdong, covering an area of 15,000 square meters, with more than 150 employees.
The sales headquarter and product developing center is located in downtown Foshan, with 1200 square meters office space. A group of innovative and passionate people work here, delivering good service and designing creative down light led products.
Diva focus on designing and manufacturing LED downlights, all downlights strictly meet the fire safety and electrical safety requirement of lighting, as our goal is to making home a better and safer place. Acquiring OHSAS18001:2007 and ISO14001:2004 certifications prove our commitment to the society and environment. Diva's lighting products are manufactured in accordance with the CE, EMC, ENEC, UL and RoHS standards. All lighting products integrate and utilize high quality electrical components such as driver from TRIDONIC and light source from CITIZEN, BRIDGELUX and CREE.
Aiming at "Becoming an outstanding innovative lighting company", Diva spare no effort on the research and development of lighting products, and has own more than 280 patents both in China and abroad, including Europe and North America. With good reputation, Diva put customers on the first place, and is dedicated to bring customers good experience by delivering good customer service, innovative products and ensure quality stability.
Our Mission: Helpin customers with business success, Working for a safer and better world.
Our Value: Satisfy customer. Pragmatic innovation. Fast&Efficiency. Open&Cooperation.
Our Vision: Create the industry's first product and become the first brand in the segment field.
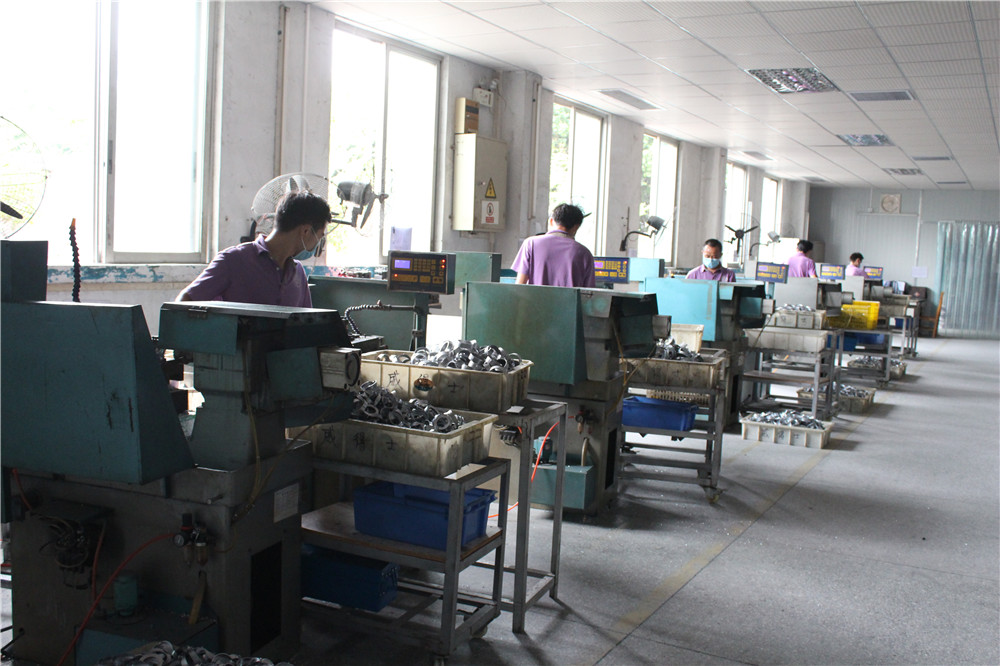
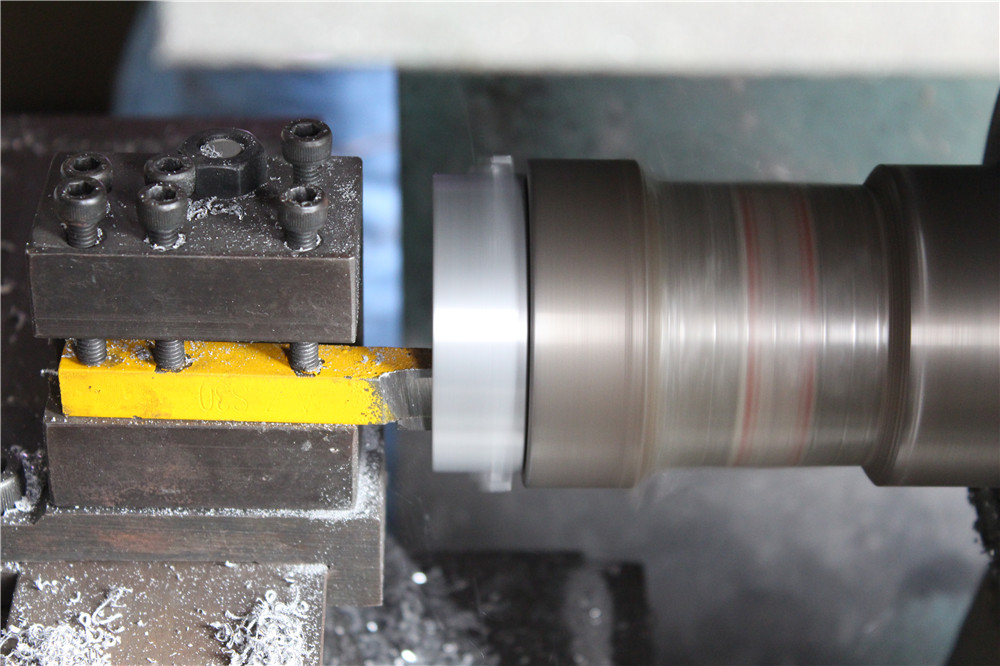
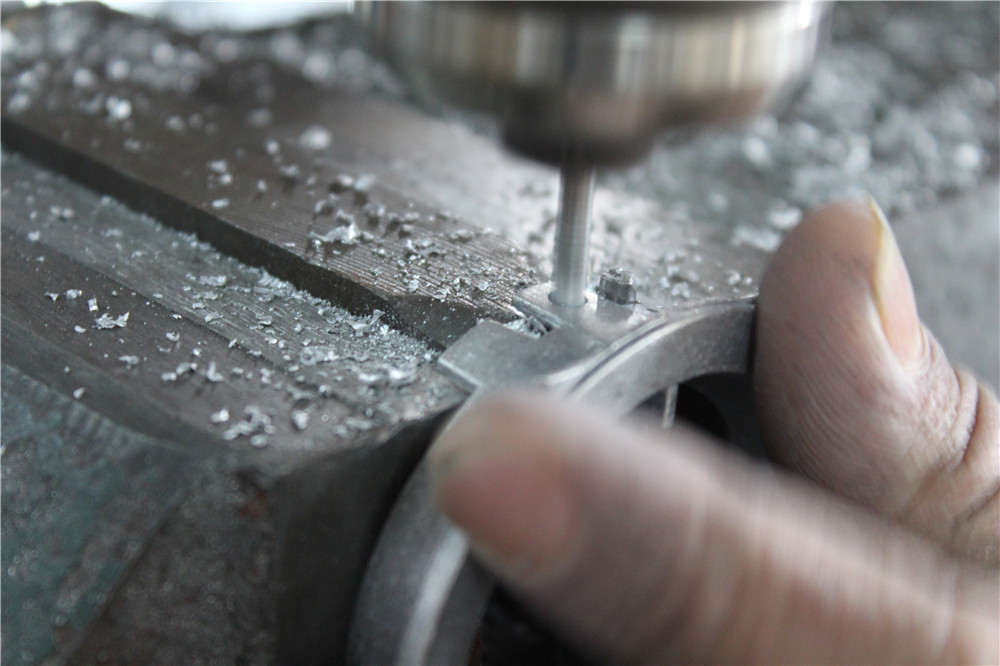
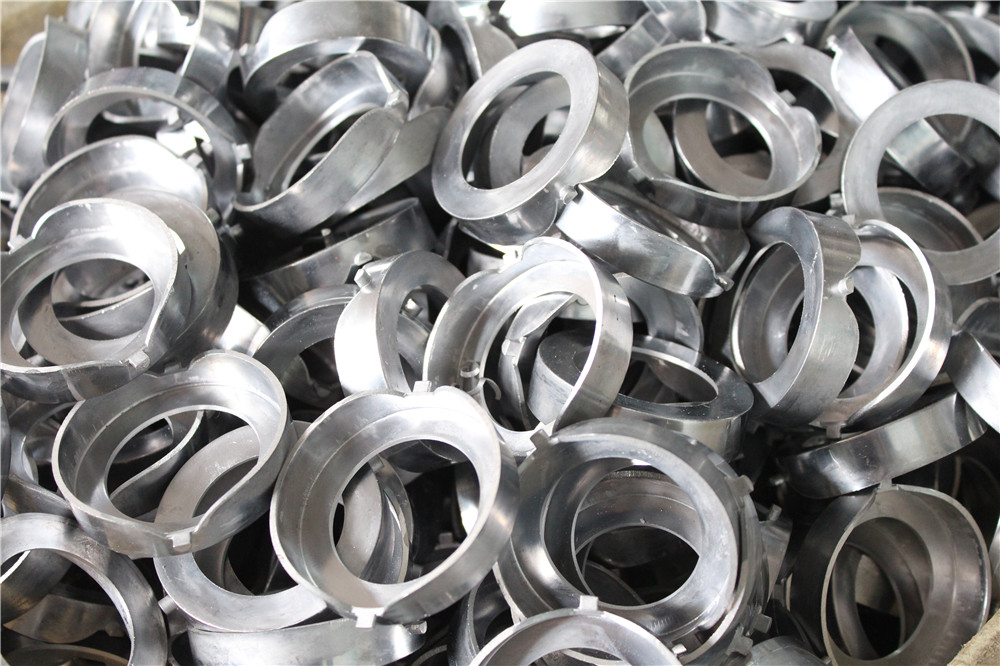
Expert answers regarding our custom OEM manufacturing capabilities, technical specifications, and international export procedures.
As a direct manufacturer with a 15,000 square meter facility, we offer flexible MOQ structures tailored to project scales. Standard OEM customization for housing color, branding, and specific driver configurations generally starts at 500 units per model, while fully bespoke optical design projects are evaluated case-by-case by our R&D engineering team.
We maintain strategic partnerships with world-renowned component manufacturers to ensure absolute reliability. Our LED drivers are predominantly sourced from TRIDONIC, and our light sources utilize high-efficiency chips from CITIZEN, BRIDGELUX, and CREE.
All our lighting products are manufactured in strict accordance with major international standards. Our portfolio holds CE, EMC, ENEC, UL, and RoHS certifications, alongside factory-level OHSAS18001:2007 and ISO14001:2004 accreditations.
Quality control is embedded at every stage—from incoming raw material inspection (IQC) and surface-mount technology (SMT) precision checks to in-process quality control (IPQC), final burn-in testing, and comprehensive outgoing quality assurance (OQA) before container loading.
Continue exploring our extensive catalog of specialized recessed, waterproof, and architectural downlights.
 Diva Lights